The Cheapest CNC Milling Cutter Supplier Is No Longer the Winning Move
2026-11-12
FREE sourcing support for qualified business buyers comparing die/mold facing cutters, with an eligible benefit of up to 3%. Eligibility applies to qualified business buyers and is confirmed after we review your product, quantity, destination, and sourcing requirements.
Procurement brief
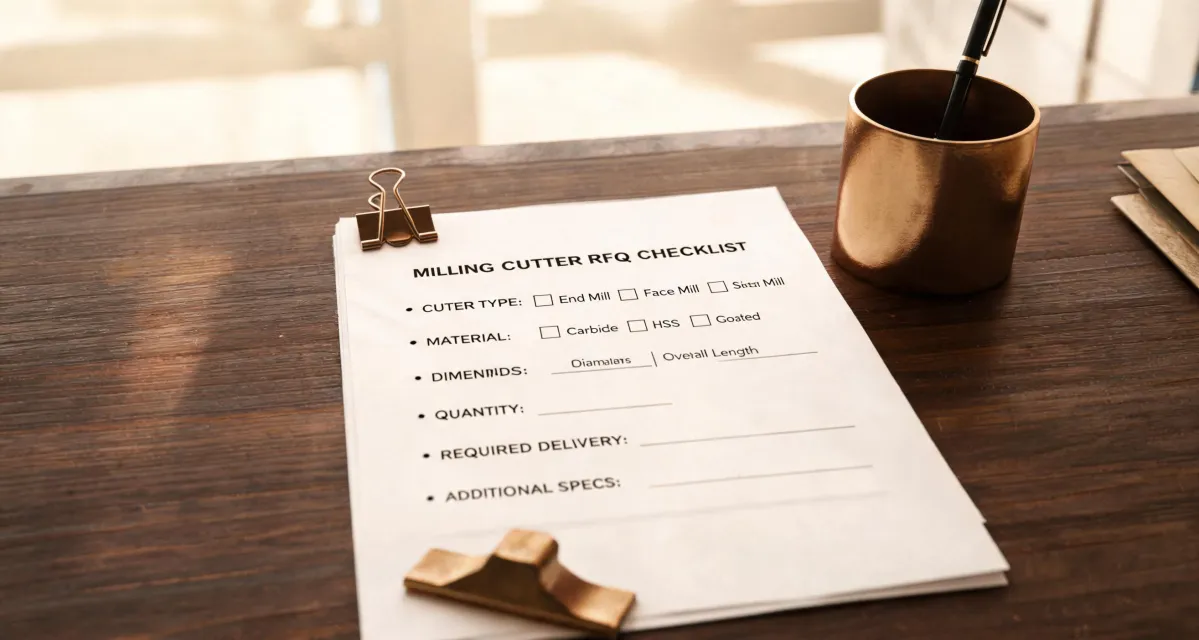
Most shop-floor emergencies on the machining side aren't actually emergencies.
I'm a production scheduler at a custom machining company. In the past nine years I've pushed through 200+ rush jobs, from 36-hour deadlines to same-week rescues on custom tooling. And when I trace those jobs backward — really trace them — the pattern is depressing. A lot of what gets called "urgent" is really a normal CNC milling cutter suppliers sourcing task that somebody sat on for six days and then dropped into my lap with a delivery date already blown.
Here's my position, plainly: whether your shop survives a rush job depends less on having a fast cutter supplier and more on how you run CNC milling cutter supplier sourcing day to day — as a deliberately efficient system or as a series of panic purchases.
Let me be more precise. Early in my role I believed rush orders demanded rush solutions — call a vendor, pay a premium, pray. That habit burned me in my fifth year. Now I see it the other way around: the smoothest rush turnarounds I've handled came from shops that had already done the sourcing work months earlier. Not from vendors anybody found at 9 p.m.
It's tempting to think a rush order is a different animal — that it needs "sprint-mode" suppliers, expedited channels, someone who answers emails at midnight. But in my experience, that's not really what happens.
Rush orders amplify whatever flaws your standard process already had. If your CNC milling cutter supplier normally takes two days to send a quote, they will still take two days under deadline pressure — except now those days cost you an idle spindle (and overtime). If your procurement side has spent years conflating "in stock" with "available on demand," a rush job will surface that distinction within an hour.
I've noticed a pattern: the shops with the smoothest rush operations don't have a faster supplier. They have a better everyday process. They know which cutters are commodity items and which are custom. They know a face milling cutter manufacturers standard lead time runs 4–6 weeks for non-catalog bodies (as of early 2025, based on published quotes — verify current windows with each vendor). And they don't burn twenty hours a week re-evaluating the same three vendors for every non-standard tool.
Which brings me to my steady position on this: a more efficient process makes an enormous difference between a cold start and a warm start.
Here's the counterintuitive part.
I've watched plenty of buyers chase the person who answers a quote fastest when a rush order lands. And in a lot of cases, the quickest responder — the one who replies in an hour and promises "in stock, ships tomorrow" — is the least suitable vendor for anything complex.
In the CNC milling cutter suppliers market, quick quotes exist because the product line is standardized (fixed diameters, coatings, grades). The moment your request drifts off a standard 4-flute flat end mill — a non-standard flute length for a specific material, a custom neck, a modified face mill body — the fast vendor will often either decline, accept with an uncertain lead time, or misread the spec.
The end milling cutter manufacturers I actually trust tend to quote a bit slower. They need to see your drawing, confirm material compatibility, and maybe steer you off a coating that will fail at your cutting speed. That slower process is frequently the only one that survives pressure.
So when a rush job is on the line, I'd rather rely on a supplier I've already vetted than a stranger I found an hour ago. Efficiency and speed aren't the same thing.
On rush jobs, the gap between the quote and the purchase order is where most failures actually happen.
Internal records at our shop showed something I found genuinely surprising (though I might be misremembering the exact percentages): the largest chunk of wasted rush time wasn't in manufacturing or transit. It was the RFQ cycle — the days between "send inquiry" and the point where I could actually place an order with confidence. The back-and-forth on specs, the missing pieces of information, the emails that didn't resolve anything.
If you only compare unit prices across several milling cutter manufacturers, you're skipping the whole tool efficiency in the fastest segment. What you should compare is clarity-from-inquiry-to-production. Some vendors can give you a spec-ready quote within two hours; others send a PDF that assumes everything from freight terms to implicit minimum order quantities.
On normal lead times, this is just annoying. On a rush job, it's catastrophic.
Of course it does. I have decade-long relationships with an end milling cutter manufacturer that I can call on a Saturday, and that matters more than any spreadsheet.
And to be fair, custom tooling has its own pace. If you're sourcing a bespoke flute profile from a small end milling cutter manufacturer with a four-person floor, a 5-week lead time is normal. That isn't an efficiency failure — it's a physics fact.
Which is exactly why I keep insisting on separating the two categories. Standard catalog cutters want efficient, systematic sourcing. Custom tools want relationships and pre-communication and a clear understanding of who can actually make what. Mixing them into one process is the real source of chaos. And if your sourcing process can't tell a commodity cutter from a non-standard one, the problem isn't the supplier — it's the process.
I don't think traditional relationship-based buying is obsolete — but I've watched plenty of "good relationship" suppliers that structurally can't meet the efficiency requirement. Both facts can be true.
Rush orders test how well a shop manages its supply chain under pressure — not how aggressively it reacts. If your CNC milling cutter suppliers sourcing work is done properly — meaning you know your inventory, you know your standard specs, you know which face milling cutter manufacturers can actually deliver, and you know which custom items need to be raised early — then the rush order is going to cost you far less time than it costs your competitor who's frantically rifling through catalogs and cold-calling vendors.
That's the part of the cutter business nobody can copy from you. Competitors can buy the same spindle and the same toolholders — but they can't buy the supplier sourcing system that's already running in your shop.
The 'emergency supplier' everyone talks about mostly isn't a different vendor. It's just a well-built process doing what it was always meant to do.
Comments are moderated. Do not send drawings here; use the RFQ form.